ADSD Consulting Private Limited

From Coconut Shell to High-Performance Activated Carbon
Discover Our Steam & Temperature Controlled Activated Carbon Manufacturing Process. From Carefully Selected Coconut Shells to Carbonisation Process To Steam Activation, Screening, Grading, Quality Testing and Final Packing. Our Activated Carbon Manufacturing Process is Designed To Deliver Consistent Pore Structure, Adsorption Performance, Purity and Quality Across Every Batch.
High Microporosity | High Hardness | Steam Activated | Consistent Quality
Activated Carbon Manufacturing Process
Premium Coconut Shells
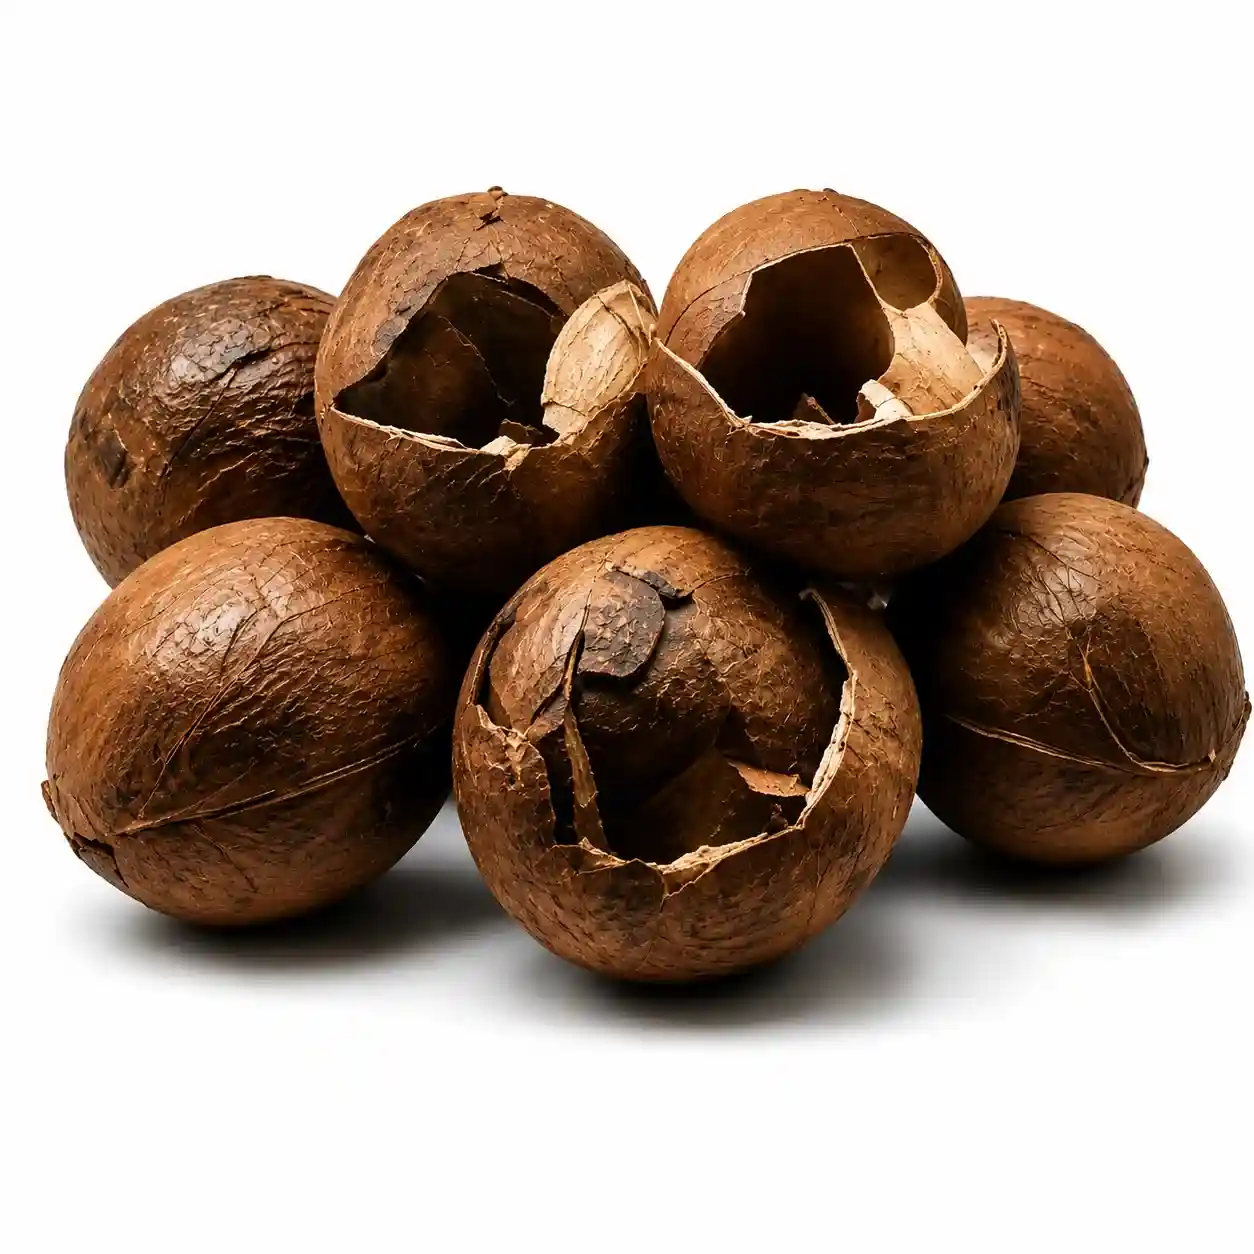
Carefully Selected Premium Quality Higher Thickness Coconut Shells Sustainably sourced for Consistent Quality.
Carbonisation
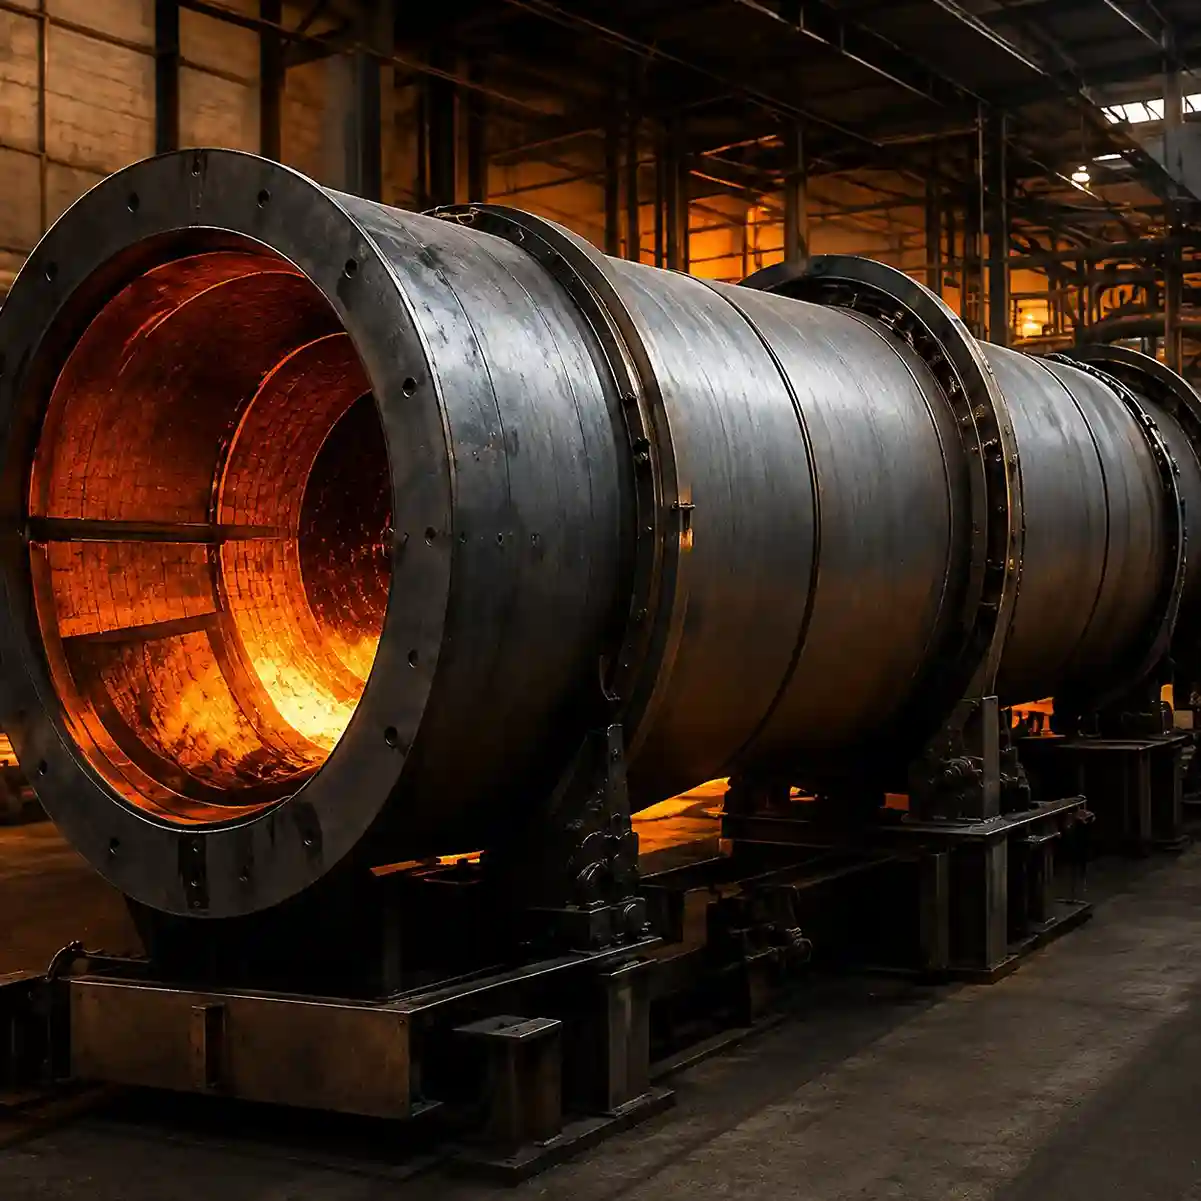
Coconut Shells are Carbonised in a Air Controlled Environment to Produce Dense Carbon Char.
Steam Activation
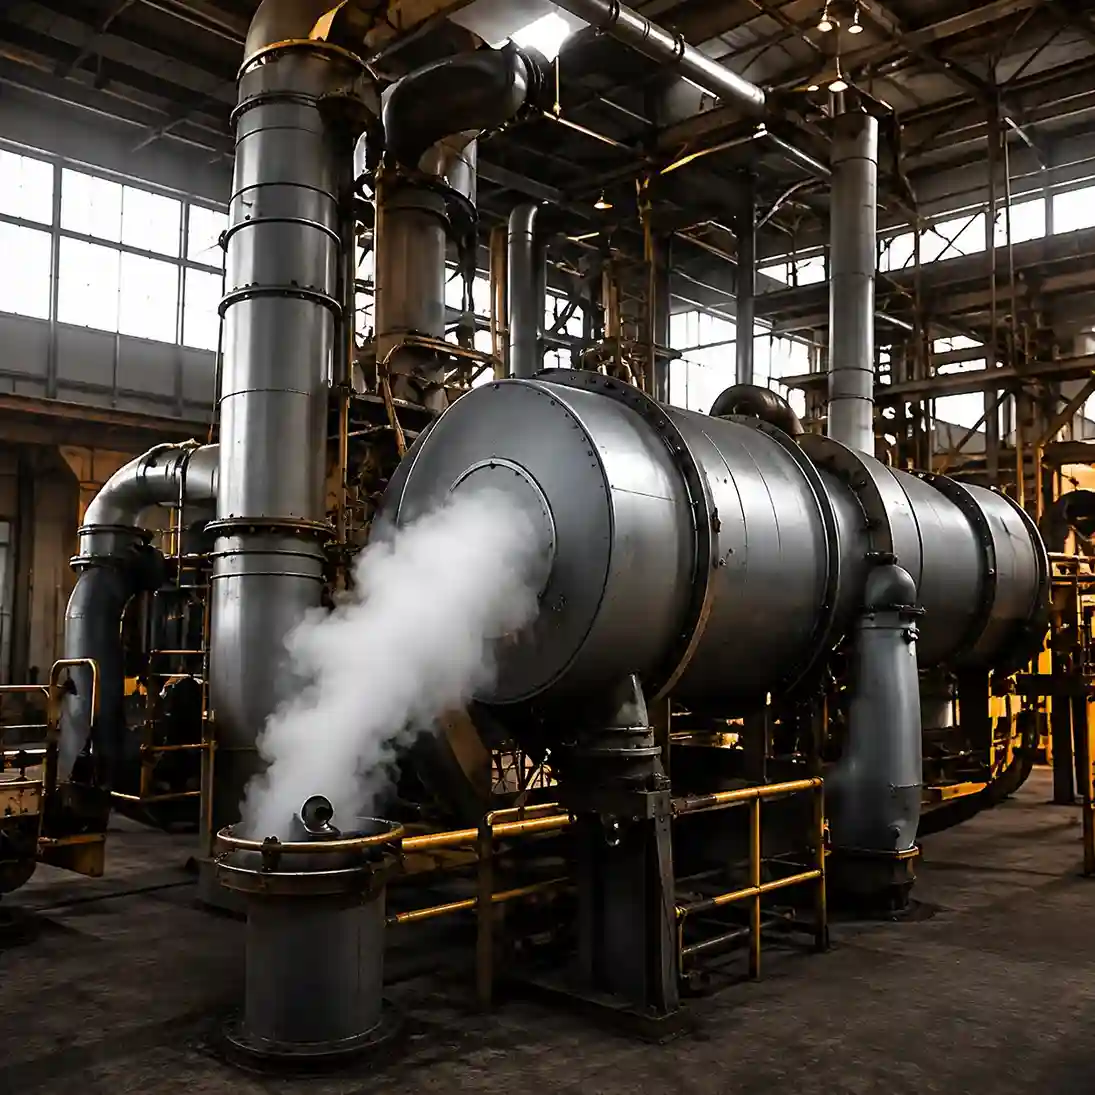
Carbon Char is Activated with Steam at 900–1000°C to Develop a Highly Microporous Structure.
Screening & Grading
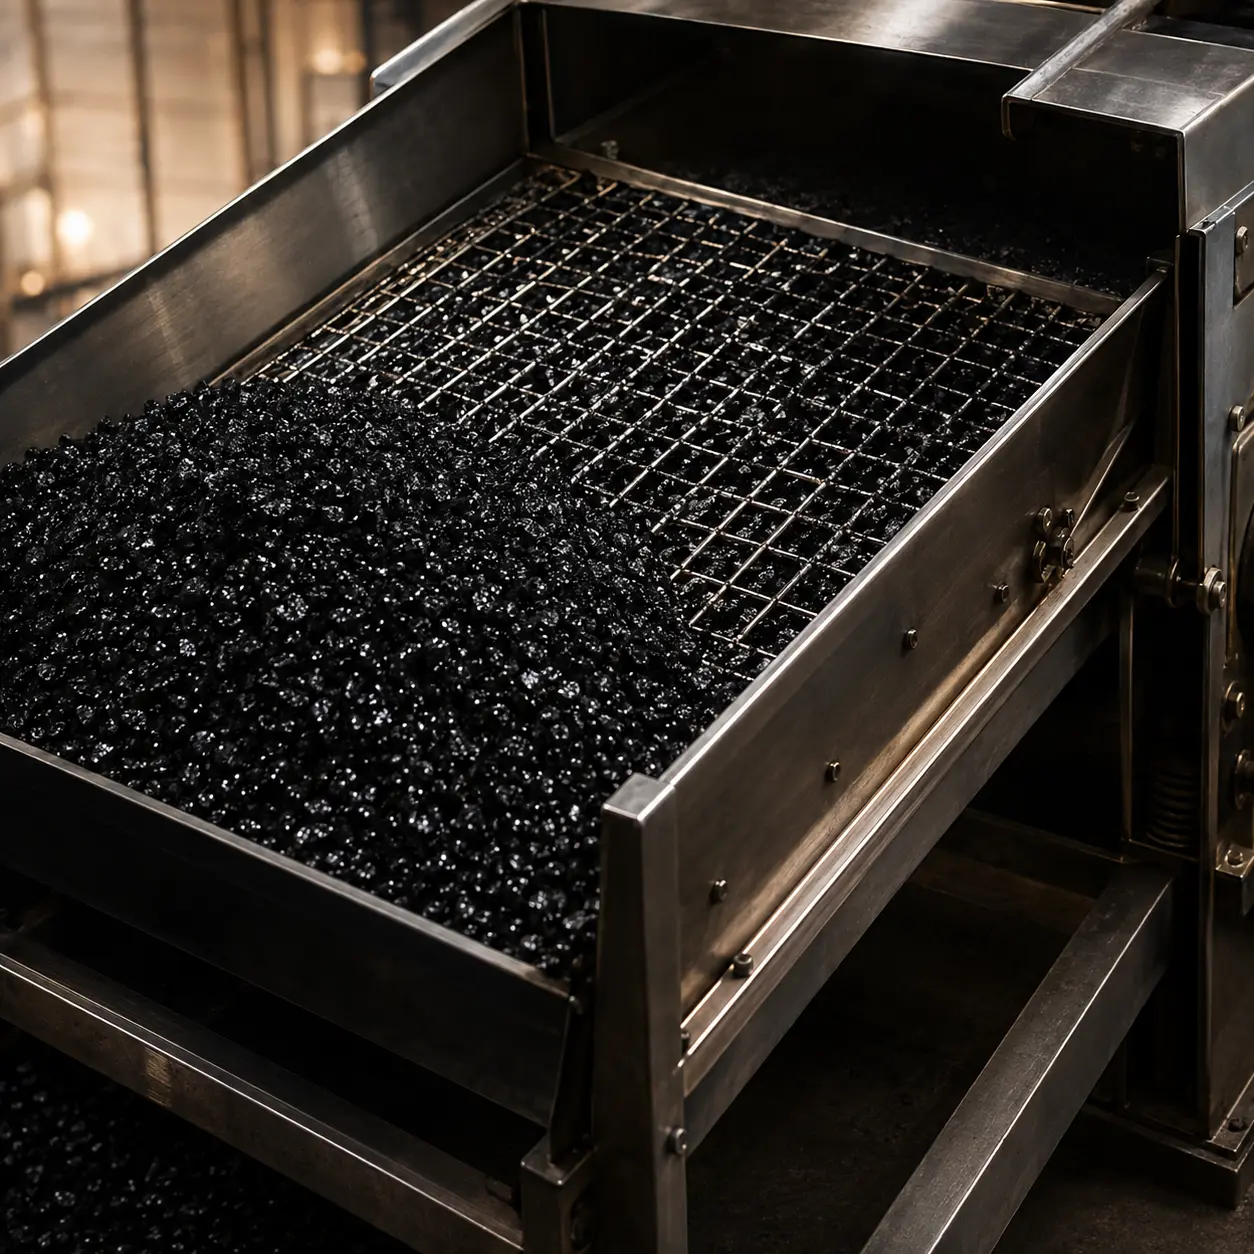
Activated Carbon is Destoned, Screened and Graded to Achieve the desired Particle & Mesh Size.
Quality Testing
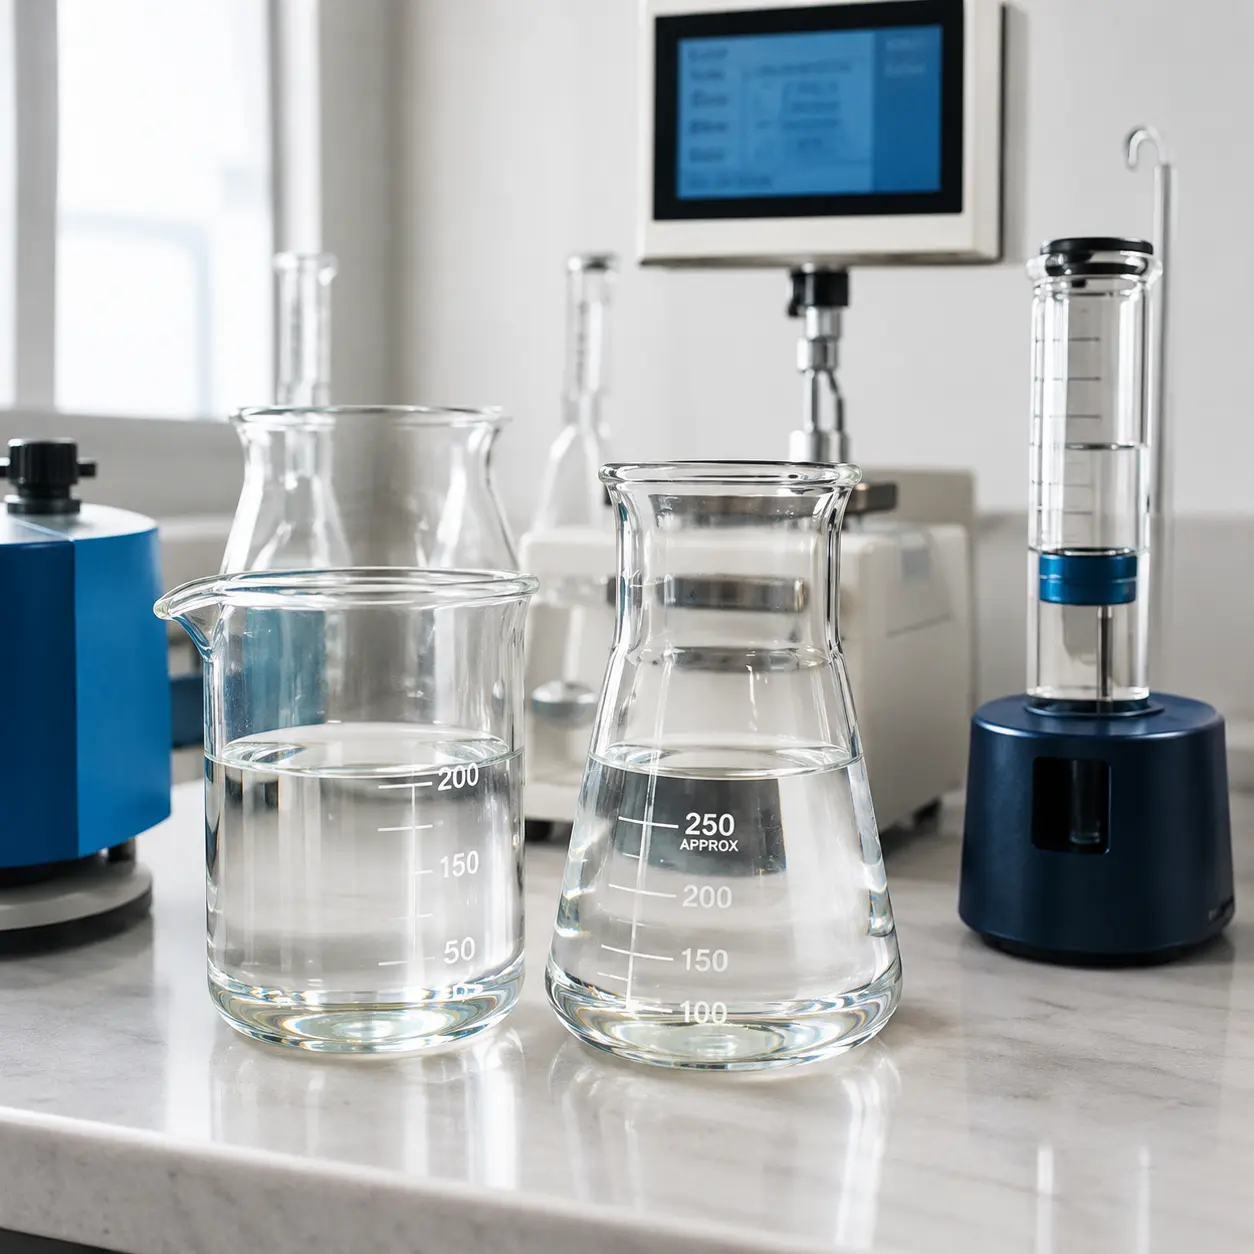
Each Production Batch is Quality Tested to ensure High Purity, Consistency and Reliable Performance.
Packing & Dispatch
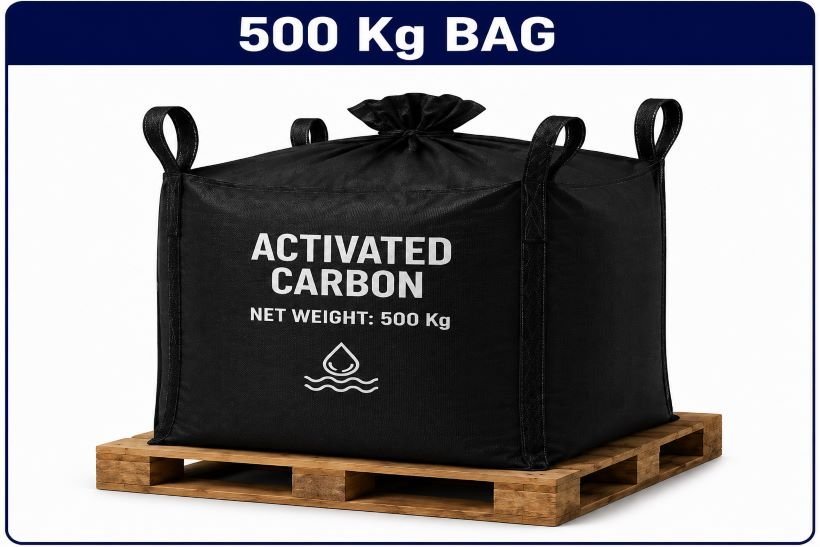
Final Product is Packed as per ADSD Standard Packaging or Clients Customized Design in 25 Kg Bags, 500 Kg/ 600 Kg Jumbo Bags.
Why Coconut Shell Activated Carbon
Coconut Shell is one of the best raw materials for making Activated Carbon – not bychance, but its structure gives superior performance compared to coal or wood.
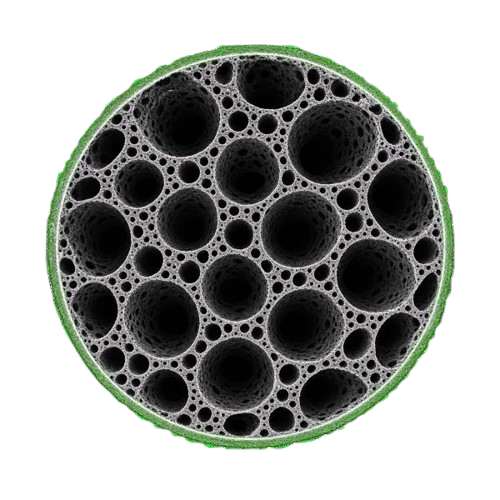
High Miroporosity (better adsorption):
After Steam Activation, Coconut Shell Develops more Microspores while removing small Molecules and ensuring High Efficiency and Adsorption.
Eco-Friendly
Source:
Produced from Renewable Coconut Shells,
making it a Sustainable and Environmentally responsible
Choice.
Higher Hardness &
Durability:
Ensures Minimal Attrition
and Longer Operational Life, especially in demanding
applications like Gold
Recovery.
Regenerable & Cost-Effective:
Can be Thermally Reactivated, Improving Lifecycle Economics. We don't just Manufacture Activated Carbon, we Deliver a Promise of Purity, Performance and Reliability.
ADSD Adsorbents & Specialities Private Limited manufactures and supplies Coconut Shell-Based Activated Carbon for customers across India and International Markets. Our Activated Carbon Manufacturing Process in India is supported by controlled production practices, quality-focused operations and application-specific product requirements. We work with Industrial Buyers, and Businesses requiring consistent Activated Carbon Products for Water Treatment, Gold Recovery, Air Purification, Pharmaceuticals, Food & Beverage, Oil & Gas and Industrial Filtration Applications. Our focus on Product Quality, Reliable Supply and Customer Specifications enables us to support diverse Activated Carbon requirements across Domestic and Global Markets. For additional industry information, the Activated Carbons Producers Association (ACPA) provides technical resources related to Activated Carbon production and applications.
ADSD Adsorbents & Specialities Private Limited also supports customers with Activated Carbon Products tailored to specific application requirements, including different grades, particle sizes and packaging formats. Our manufacturing and quality-focused approach helps maintain consistency across production batches while meeting customer specifications. From standard industrial requirements to application-specific Activated Carbon Solutions, we work closely with customers to understand their technical requirements, quantity, packaging and delivery schedules. This approach enables ADSD to provide dependable Activated Carbon Supply Solutions for Water Treatment, Gold Recovery, Air Purification, Pharmaceuticals, Food & Beverage, Oil & Gas and other Industrial Applications across Domestic and International Markets.

About Us
ADSD Consulting Private Limited
ADSD Adsorbents & Specialities
Private Limited
Delivering integrated Engineering, EPC, Consulting, Chemicals & Supply Chain and Activated Carbon solutions to Industries Worldwide.
Engineering & EPC Business
Chemicals & Supply Chain Business
Contact Us
- info@adsd.in
- +91 9958582437
-
Anthurium Office Space, 1103-1105, Sector-73, Noida,
Pin 201307, NCR Delhi, India
Download Brochure

About
ADSD Group, headquartered in Noida/Delhi (NCR), India, ADSD Group began its journey in 2017 with the establishment of its flagship company ADSD Consulting Pvt. Ltd.
Engineering & EPC
Supply Chain
Activated Carbon Business
Quick Link
Contact Us
- info@adsd.in
- +91 96506 93468
-
Anthurium Office Space, 1103-1105, Sector-73, Noida,
Pin 201307, NCR Delhi, India
Download Brocher
Copyright © 2026 All rights reserved. Powered by ADSD Group