ADSD Consulting Private Limited
Applications of activated carbon

Applications of Activated Carbon span a wide range of Industrial, Environmental and Process Applications, supporting effective Adsorption, Purification and Contaminant Removal. Our Activated Carbon Solutions help remove Impurities, Odors, Colors, Organic Compounds and Unwanted Contaminants from various process streams. With applications across Gold Mining, Water & Wastewater Treatment, Air & Gas Purification, Food & Beverage, Pharmaceuticals, Chemicals and Industrial Processes, we support cleaner and more efficient operations. Our solutions are designed to meet diverse Industrial Requirements, delivering Consistent Performance, Process Reliability, and Improved Product Quality.

Purification • Filtration • Adsorption • Process Enhancement

Water | Air & Gas | Industrial | Food & Beverage | Pharmaceutical

Activated Carbon is widely used in Gold Recovery to adsorb dissolved gold from cyanide-based solutions. It is commonly used in CIP, CIL, and CIC processes for efficient recovery and reliable carbon performance.

In Water Treatment, Activated Carbon helps remove Organic Contaminants, Chlorine, Taste, Odor, Color, and Trace Pollutants from drinking water, process water, and wastewater, supporting cleaner and safer water.

Activated Carbon provides effective Air Purification by capturing VOCs, Hydrocarbons, Solvent Vapors, Odors, and Other Gaseous Contaminants, helping improve air quality and industrial process performance.

In Oil & Gas Purification, Activated Carbon helps remove VOCs, Organic Compounds, Odors, and Trace Impurities from hydrocarbon and process streams, supporting efficient purification and improved product quality.

Activated Carbon is used in Pharma & Intermediates for purification and decolorization. It helps remove Organic Impurities, Color Bodies, and Trace Contaminants, supporting consistent product quality.

In Food & Beverages, Activated Carbon supports purification and decolorization while helping remove Organic Compounds, Chlorine, Taste, and Odor for improved product quality and process performance.

Gold Recovery

Water Treatment

Air Purification

Oil & Gas
Purification

Pharma & Intermediates

Food &
Beverages

Applications of Activated Carbon for Global Industrial Requirements

Applications of Activated Carbon extend across a wide range of Industrial, Environmental and Process Applications where effective adsorption, purification and contaminant removal are required. ADSD Group provides reliable Activated Carbon Solutions for customers across Global Markets, supporting diverse requirements with suitable grades and dependable supply.

Choosing the Right Activated Carbon for Your Application

Selecting the right Activated Carbon depends on Process Conditions, Contaminants, Adsorption Performance and Operating Requirements. Different applications may require specific Particle Size, Mesh Size, Surface Area, Iodine Number, Hardness and Ash Content.

ADSD Group offers Activated Carbon Products including Granular Activated Carbon, Powdered Activated Carbon, Pelletized Activated Carbon and Acid-Washed Activated Carbon for diverse Industrial and Environmental Applications.

For Water & Wastewater Treatment, Gold Recovery, Air & Gas Purification, Oil & Gas, Food & Beverage and Pharmaceutical Applications, suitable carbon grades can be selected according to specific process and purification requirements.

Our focus is on Product Quality, Application Suitability, Consistent Performance and Reliable Supply. We support customers with suitable Activated Carbon Grades based on their technical specifications and application needs.

Through our Global Supply Network, ADSD Group provides dependable Activated Carbon Supply Solutions for customers across International Markets, supporting different product quantities, specifications and delivery requirements.

For additional technical information on activated carbon in drinking water treatment, refer to the U.S. Environmental Protection Agency (EPA) resource on drinking water treatment technologies.

Applications Of Activated Carbon

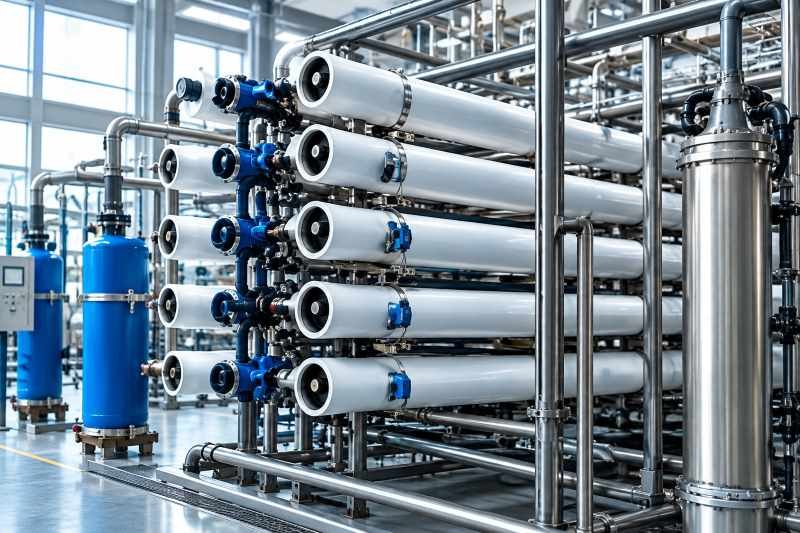
Desalination & RO Pre-Treatment

Activated Carbon protects RO membranes by removing chlorine, chloramines, VOCs, THMs and other oxidizing agents before filtration. It reduces organic fouling, extends membrane life, and improves overall system efficiency and performance. Suitable for both POU (Point of Use) and POE (Point of Entry) water treatment applications.
Applications Of Activated Carbon

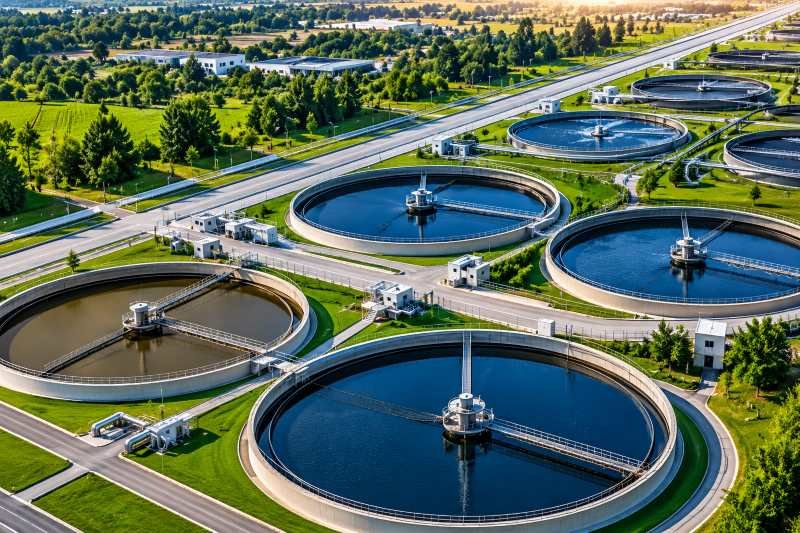
Wastewater Treatment (Industrial & Municipal)

Activated Carbon improves industrial and municipal wastewater quality by efficiently removing pollutants before discharge or reuse. It supports final polishing and enhances treated water performance.
Applications Of Activated Carbon

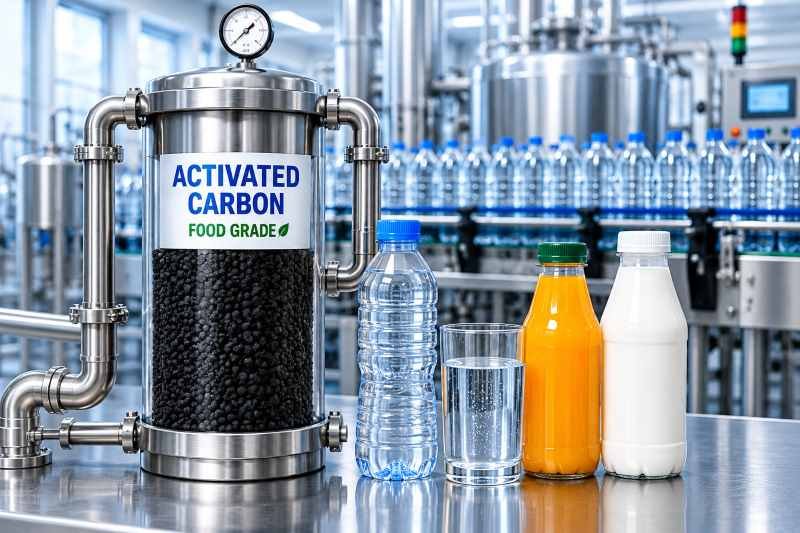
Food & Beverage Industry

Activated Carbon ensures high-purity water quality for food and beverage production with food-grade performance and low ash content. It effectively removes taste, odour and chlorine, purifies process water and supports decolourization in liquid processing.
Applications Of Activated Carbon

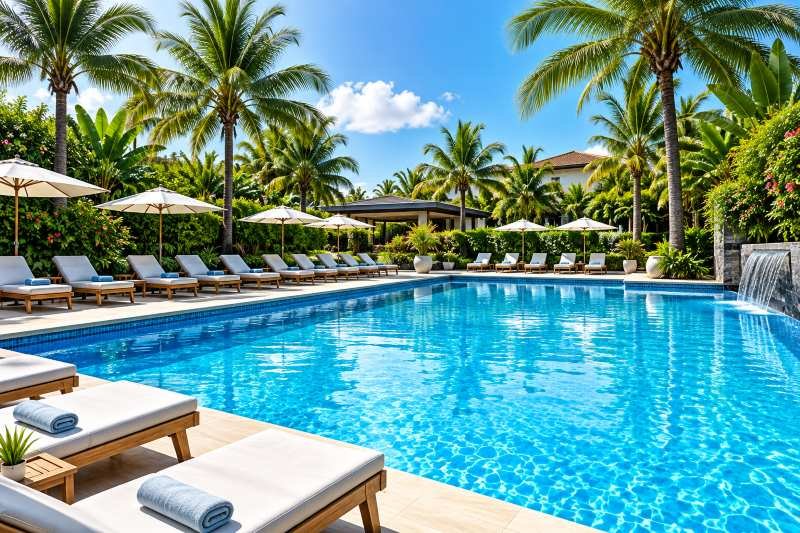
Swimming Pool & Recreational Water Treatment

Activated Carbon improves water quality, safety and user comfort by removing chlorine by-products, controlling odour and enhancing water clarity and aesthetics.
Applications Of Activated Carbon

Aquaculture & Aquarium Water Treatment

Activated Carbon maintains clean, safe and healthy water conditions for aquatic life through natural, residue-free filtration. It effectively removes toxins, organic waste, odour and discoloration for improved water quality.
Applications Of Activated Carbon

Bottled Water & Beverages

Activated Carbon ensures consistent taste, quality and regulatory compliance in bottled water and beverage production. It is widely used in carbonated drinks and fruit juice processing to maintain taste, colour and aroma consistency while removing residual impurities.
Industry Applications

Gold Recovery


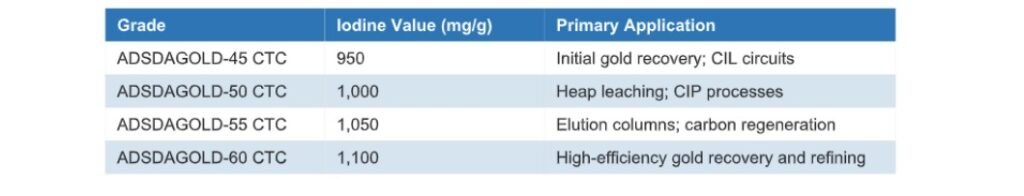
ADSD Adsorbents produces premium coconut shell–based activated carbon specifically engineered for Carbon-in-Pulp (CIP), Carbon-in-Leach (CIL), and Carbon-in-Column (CIC) circuits in gold mining operations. With superior adsorption kinetics, high mechanical strength, and minimal attrition loss, our products are designed to maximise gold recovery yields, extend service life, and reduce operational costs, making them the preferred choice for the most demanding mining environments.

Applications Of Activated Carbon

Gold Cyanidation Process

Gold cyanidation is a widely adopted hydrometallurgical process for extracting gold from ore. Crushed and milled ore is treated with a dilute cyanide solution, forming a soluble gold-cyanide complex. Oxygen is introduced to enhance leaching efficiency and accelerate the dissolution reaction. The dissolved gold is subsequently recovered using activated carbon through one of three principal adsorption processes: CIP, CIL, or CIC. The loaded carbon is then processed through elution and refining to recover the final gold product.

Carbon-in-Pulp (CIP)

• Gold is first leached from the ore using a cyanide solution, producing a gold-bearing slurry.

• The slurry is contacted with activated carbon in a series of dedicated adsorption tanks.

• Leaching and adsorption are conducted as separate, sequential stages, enabling precise process control and optimised recovery efficiency.

• Activated carbon flows counter-current to the slurry, maximising gold loading and adsorption performance.

• The loaded carbon is subsequently eluted, regenerated, and returned to the process, ensuring cost-effective continuous operation

Carbon-in-Leach (CIL)

• Cyanide leaching and gold adsorption are integrated into a single, concurrent stage.

• Activated carbon is introduced directly into the leaching tanks, enabling simultaneous gold dissolution and adsorption.

• This streamlined approach reduces equipment requirements, lowers capital expenditure, and shortens processing time.

• Particularly effective for ores with rapid leaching characteristics, ensuring fast, efficient gold recovery.

Carbon-in-Column (CIC)

• Commonly applied in heap leach operations for the recovery of gold from low-grade deposits.

• Crushed ore is stacked on lined leach pads and irrigated with a cyanide solution to dissolve gold.

• The gold-bearing solution is passed through columns packed with activated carbon, where gold is effectively adsorbed.

• Loaded carbon is periodically removed for elution and regeneration, enabling continuous, uninterrupted operation.

Technical Advantages of ADSD Gold Recovery Carbon

• High Resistance to Attrition — Minimises particle breakdown during continuous agitation in CIP and CIL circuits.

• Excellent Gold Retention — Ensures maximum adsorption efficiency and minimal carbon loss during the elution process.

• Superior Mechanical Hardness — Provides outstanding structural strength, reducing particle breakage and extending service life.

• Low Dust and Ash Content — Delivers cleaner operations, reduces system contamination, and enhances overall adsorption efficiency.

• Very Low Platelet Content — Ensures uniform particle structure, improving flow dynamics and adsorption performance.

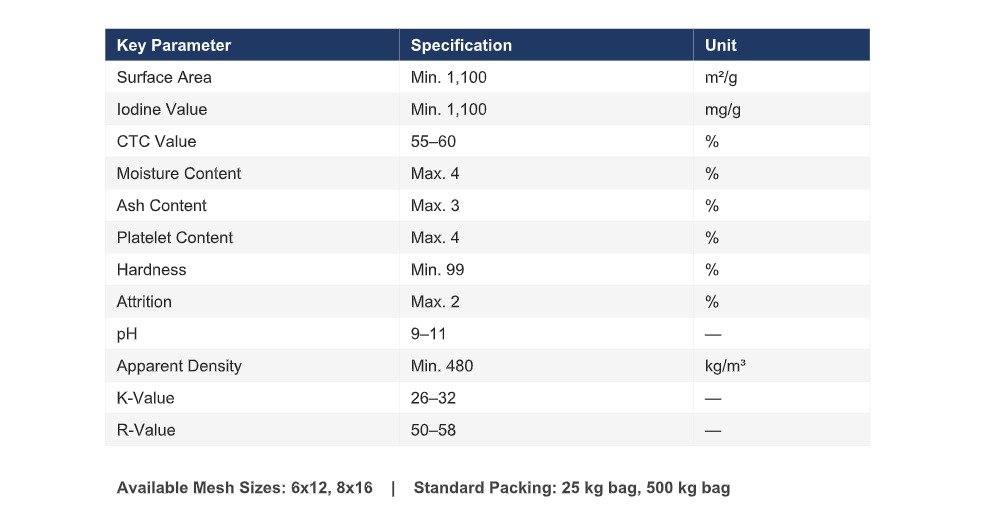
Gold Recovery — Product Specifications

Applications Of Activated Carbon

Grade Comparison — Gold Recovery

Applications Of Activated Carbon